Sumitomo Electric Wiring Systems

Quality Leadership

Quality is built at the station, not inspected at the end. Each topic follows the same PDCA loop, backed by line data.

PPlanDDoCCheckAAct
PDCA · Defect ratio ownership on Toyota and PSA harnesses assembly lines

My Quality Leadership Approach

Zero defects is a team habit

8–9
zero-defect teams per week
0.07%
best assembly line DR, WK45
0.09%
assembly lines DR, WK45
#1
SEWS quality ranking, 61 sites
PPlan

Defect-ratio target per line and per team; every defect logged by team, station and cause.

DDo

Daily defect discussion on the line; abnormality forms; stop and escalate when equipment lets defects pass.

CCheck

Weekly defects-per-team trend and worst line / worst defect review.

AAct

Countermeasures become jigs, training and standards; best practice shared across teams and sites.

Assembly production lines defect ratio (%)

Target 0.16%ActualOut of target
0.20%0.15%0.10%0.05%0.00%WK34WK35WK36WK37WK38WK39WK40WK41WK42WK43WK44WK450.17%0.18%
Across about 40,000 harnesses a week, the assembly lines stay near 0.1% defect ratio; only WK35 and WK39 went above the 0.16% target.
PDCA · Pipe line defect reduction · Green Belt DMAIC · July 2022

Root Cause Analysis

From 178 defects to their root causes

178
defects in the July baseline
13 → 1
damage component, team A
4.93 → 5.22σ
sigma level, baseline → target
2.1% → 1.5%
defect ratio, baseline → target
PPlan

July baseline: 8,379 harnesses, 178 defects, yield 99.987%, 4.93σ, OEE 91%. Pareto per team (A, B, C).

DDo

Fishbone and 5 Why on the top defects: harness not fixed to the stand at insertion; jig not guiding the bender operator.

CCheck

Damage component on team A fell from 13 to 1 after the fix.

AAct

Insertion method trained, conveyor edges covered with rubber, jig marks added; targets set at 1.5% DR, 5.22σ, 91.6% OEE.

Pareto: Pipe line defects, before vs after

Before (July)After
3512Wrongdimension276Damagecomponent1910Wrongposition179Shortbranch147Damageconnector123Scratchedpipe126Openbracket95Longbranch
Wrong dimension and damage component led the Pareto, so the team attacked them first. After the countermeasures: 145 → 58 defects across the 8 types.
ProblemRoot causeCountermeasure
Damage component & scratched pipeHarness not attached to the stand correctly at insertion (station 1)Method training at insertion; rubber covers on conveyor edges
Wrong component orientationThe jig does not guide the bender operatorPosition mark on the jig; jig redesign
PDCA · Turning every fix into a standard the next shift follows

SOPs & Work Instructions

If it is not written, it is not standard

Hourly
checks on critical stations
4M
change control on every jig
6M
fishbone in each control plan
Shadow
training before new operators work alone
PPlan

Control plan per line: 6M fishbone, root causes, last-5-days target and a repair plan.

DDo

Train the right method at the station; new operators work as shadows first; hourly checks on critical stations.

CCheck

Lean audit point S4: checklists, PFUs and MOMs defined and used; abnormality forms as evidence.

AAct

4M changes (machine, jig, method, material) only through engineering; standards updated after every countermeasure.

01Abnormality found
02Stop & contain
03Report with abnormality form
04Root cause (6M)
05Update SOP / WI
06Train & verify
Wrong fork after a 4M changeNarrow fork installed by mistake; the correct wide fork restored and the change routed through engineering.
New team on Roof lineUnplanned dimension defects; the new team moved to shadow training before working alone.
Test board passing terminal back-outBoard stopped and reported to engineering; abnormality form raised as evidence.
PDCA · Jigs and vision that make the wrong way impossible

Poka-Yoke: Mistake-Proofing

Design the mistake out, don't inspect it out

5
mistake-proofing devices
3
jigs redesigned / modified in one quarter
2
connector codes covered by AI vision
PPlan

Pick defects caused by method, not by people: clip, branch length, wrong clip, bent pins.

DDo

Redesigned clip jig, restored the correct fork, added a branch-length gauge, started a jig that rejects the wrong clip, AI vision for bent pins.

CCheck

Defects tracked per team after each device; vision images reviewed at each stage.

AAct

Devices standardized on the line; ideas shared through Yokoten.
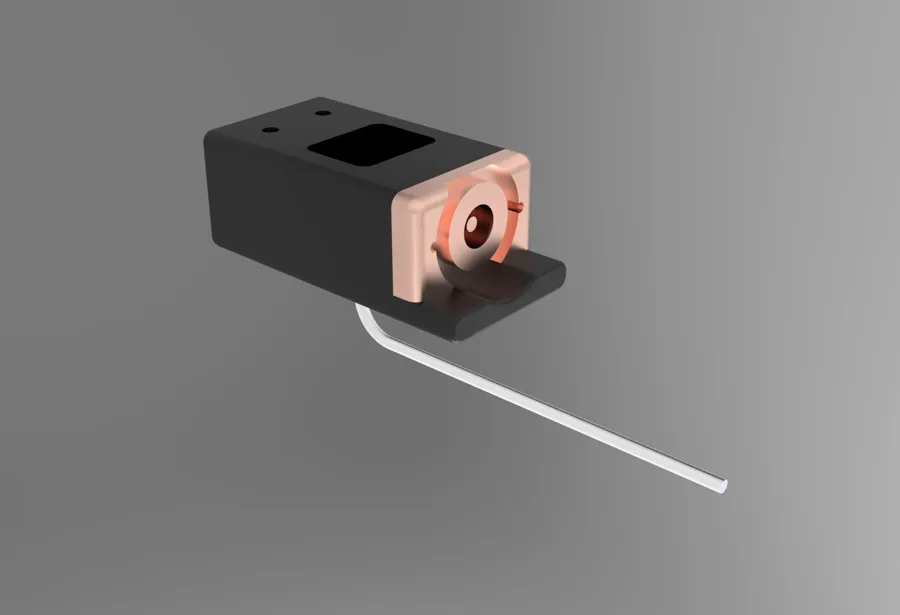
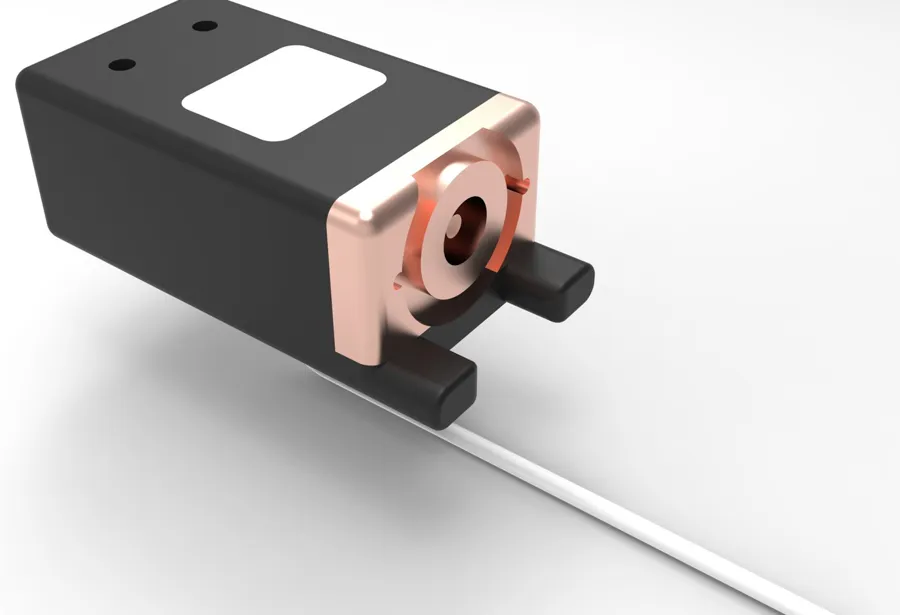
1Clip jig redesignOld jig trapped the clip tail, so operators skipped it. The new shape gives free access.
2Correct forkA narrow fork had replaced the right one; the wide fork is back under 4M control.
3Branch-length gaugeA gauge on the clip rosette fixes the branch length on PDB LHD.
4Wrong-clip-proof jigIn design: the wrong clip, used 4× in the harness, will not fit the one position meant for the right clip.
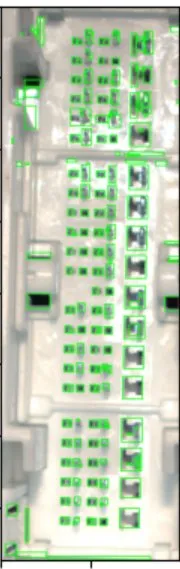
5AI bent-pin detectionVision finds connectors 521/522 even when shifted, and boxes any bent pin.
BeforeBefore: old clip jig
Before: old clip jig
AfterAfter: new clip jig
After: new clip jig
AI vision: bent pins boxed
PDCA · DOWNTIME, mapped to real actions on the line

Eliminating the 8 Wastes

Every waste had an owner and an action

8 / 8
wastes with an action
+5%
efficiency, assembly line
≈€23K
material saved per year
4 → 3
pre-blocks on Roof B618
PPlan

Walk the line with the 8 wastes in mind; quantify each with the cycle-time, defect and material data.

DDo

Act on each waste: line balancing, station merges, kitting cleanup, material trim.

CCheck

Check efficiency, defect ratio and material use week over week.

AAct

Keep what worked in the build plan and the lean audit.

WasteWhat we foundWhat we did
DefectsPipe line baseline 2.1% DRRCA + poka-yoke; damage component 13 → 1
OverproductionPack drifting from planHourly plan vs pack board
WaitingInverter 2 waits 30 s per cycleLine rebalancing with time studies
Non-utilized talentUneven operator effectivenessKaizen to raise every operator's effectiveness
TransportationKitter and tape-back as two stationsMerged on Tailgate B618
InventoryUseless parts in the PDB Left kitting areaCleared; stock level set for every part
Motion4 pre-blocks on Roof B618Same output with 3 pre-blocks
Extra processingShields cut 35 mm / 15 mm too long; extra tape issuedTrimmed to drawing; 43 → 39 tape rolls per shift