Quality Leadership
Quality is built at the station, not inspected at the end. Each topic follows the same PDCA loop, backed by line data.
My Quality Leadership Approach
Zero defects is a team habit
Defect-ratio target per line and per team; every defect logged by team, station and cause.
Daily defect discussion on the line; abnormality forms; stop and escalate when equipment lets defects pass.
Weekly defects-per-team trend and worst line / worst defect review.
Countermeasures become jigs, training and standards; best practice shared across teams and sites.
Assembly production lines defect ratio (%)
Root Cause Analysis
From 178 defects to their root causes
July baseline: 8,379 harnesses, 178 defects, yield 99.987%, 4.93σ, OEE 91%. Pareto per team (A, B, C).
Fishbone and 5 Why on the top defects: harness not fixed to the stand at insertion; jig not guiding the bender operator.
Damage component on team A fell from 13 to 1 after the fix.
Insertion method trained, conveyor edges covered with rubber, jig marks added; targets set at 1.5% DR, 5.22σ, 91.6% OEE.
Pareto: Pipe line defects, before vs after
SOPs & Work Instructions
If it is not written, it is not standard
Control plan per line: 6M fishbone, root causes, last-5-days target and a repair plan.
Train the right method at the station; new operators work as shadows first; hourly checks on critical stations.
Lean audit point S4: checklists, PFUs and MOMs defined and used; abnormality forms as evidence.
4M changes (machine, jig, method, material) only through engineering; standards updated after every countermeasure.
Poka-Yoke: Mistake-Proofing
Design the mistake out, don't inspect it out
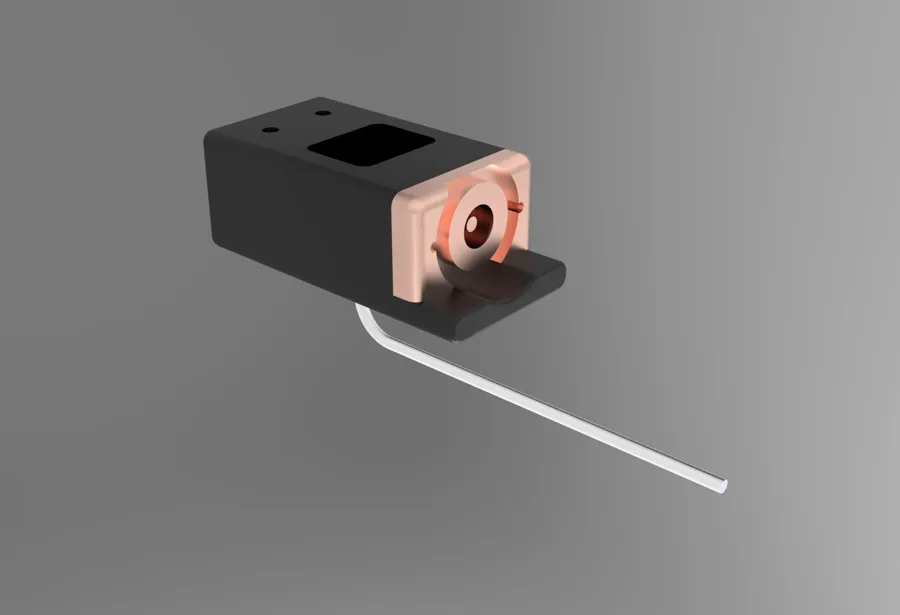
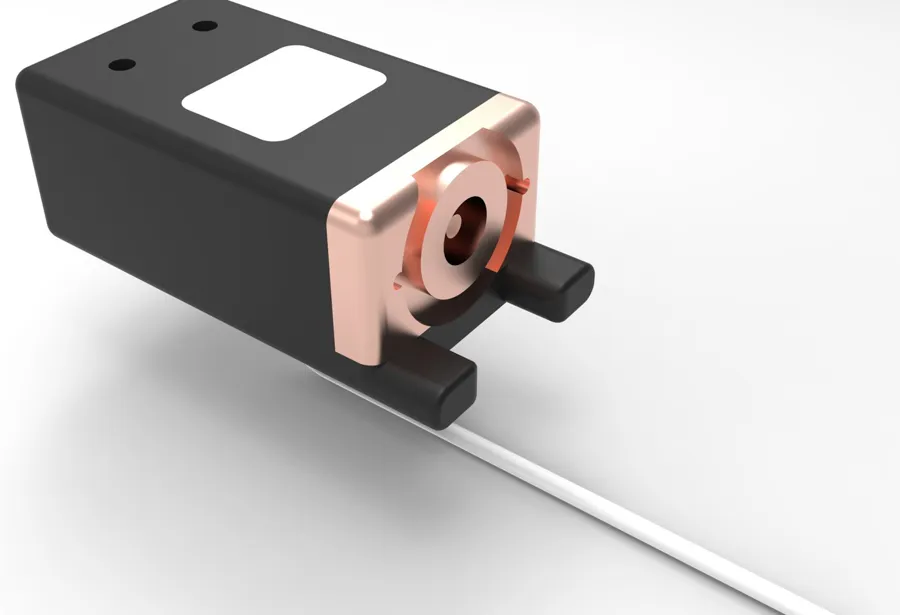
Pick defects caused by method, not by people: clip, branch length, wrong clip, bent pins.
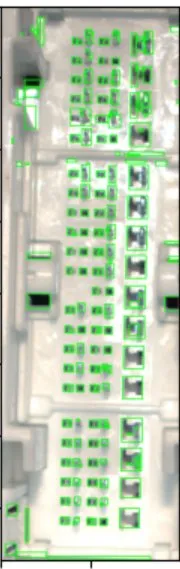
Redesigned clip jig, restored the correct fork, added a branch-length gauge, started a jig that rejects the wrong clip, AI vision for bent pins.
Defects tracked per team after each device; vision images reviewed at each stage.
Devices standardized on the line; ideas shared through Yokoten.
Eliminating the 8 Wastes
Every waste had an owner and an action
Walk the line with the 8 wastes in mind; quantify each with the cycle-time, defect and material data.
Act on each waste: line balancing, station merges, kitting cleanup, material trim.
Check efficiency, defect ratio and material use week over week.
Keep what worked in the build plan and the lean audit.