Achievements

From a state-funded graduation project that made headlines in Egypt’s leading newspapers and landed on national TV, to a Six Sigma project at Sumitomo Electric that saved €113.5K a year and lifted line efficiency by 11%, to an automated fabrication drawing system at Rollc KSA that stops errors before they reach the shop floor — every win here started with a real problem and ended with measurable results.

TV Interviews

Graduation Project: Rubber Recycling, featured on "Mostaqbal Masr" (Channel 1, Egyptian TV) and covered by Al-Shorouk, Al-Ahram, Sada El-Balad, and Al-Dostor.
Open on YouTube ↗
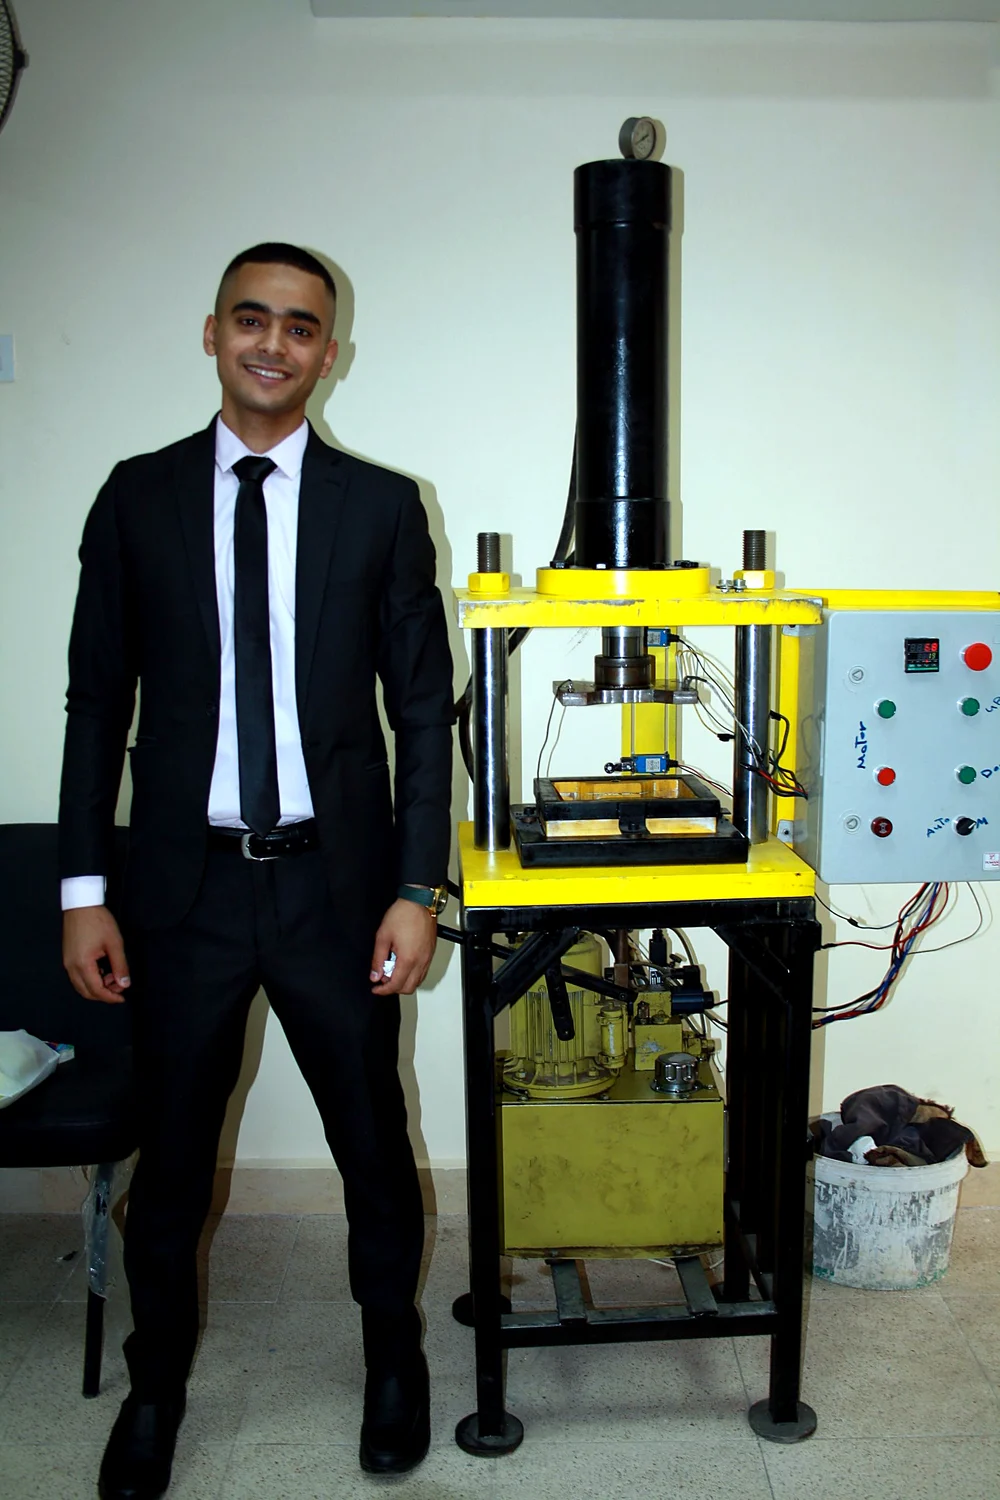
Real Picture
Ahmed standing next to his rubber recycling machine, a yellow hydraulic press with a control panel
Render video for the machine
Download Project Presentation
Six Sigma · DMAIC · Sumitomo Electric · 2023

Six Sigma Project Leader

As a Leader, I led a cross-functional DMAIC project against open anti-back defects on Toyota wire harnesses. These defects slipped past electric test boards and reached the customer as terminal back-outs. In five months we took them to zero.

0
Customer concerns after rollout (target met)
−66.5%
Downtime
#1
SEWS Group quality ranking, 61 sites, 3 months running
7
Sites adopted the solution (Yokoten)

The DMAIC roadmap

DDEFINE75% of customer concerns came from Toyota, 9 of them anti-back claims.
MMEASURESide-type connectors caused 81% of anti-back defects.
AANALYZE4M and 5 Why found two root causes: training and test-jig design.
IIMPROVEThree countermeasures; a 3-second timer jig closed the gap.
CCONTROLStandardized, validated and deployed to 7 sites.

Side anti-back defect rate, from baseline to zero

% of internal defects · Toyota CHR lines
Solution 1Training Solution 2Jig fix Solution 33 s timer 5.7% 4.8% 3.2% 2.4% 0.6% 0% BaselineMay–Jun Aftertraining TMP fixWK 34 TimerWK 35 TimerWK 36 WK 37–39zero

Analyze → Improve: root causes and countermeasures

Occurrence: training did not cover each closing method Detection: test jig (TMP) missed a 1 mm semi-open anti-back Found with 4M + 5 Why
STEP 1
Train operators

Sample board and manual for side, front and rear anti-backs, with the right closing method for each.

7%
5%
BeforeAfter
Total ABO + TBO 7% → 5%
STEP 2
Redesign the test jig

Cylinder stroke tuned to a sensor so only a closed anti-back passes, plus a weekly jig risk assessment.

4.8%
3.2%
BeforeAfter
Side anti-back 4.8% → 3.2%
STEP 3 · OUR IDEA
Two-cylinder jig with a 3 s timer

A presence cylinder finds the connector, then a spacer cylinder checks the anti-back after a 3-second delay validated with the supplier.

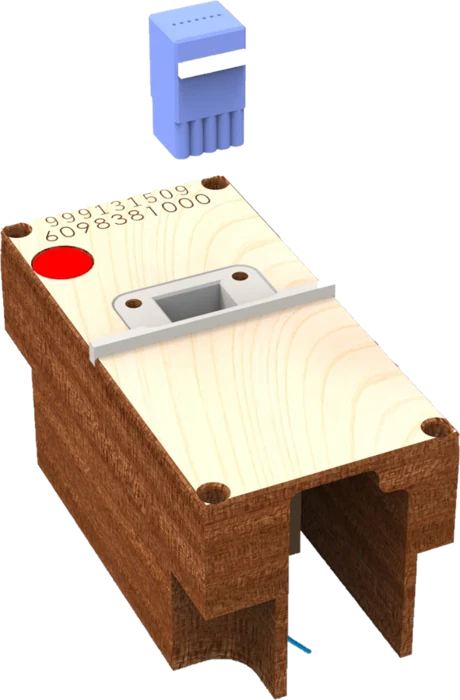
3D render of the redesigned anti-back test jig with a connector above it 3D CONCEPT
Side anti-back → 0% from WK 37
−10.75%
Scrap
Connector scrap, Jul vs Sep
−66.5%
Downtime
Test workshop, min per week
Cost
€113.5K
Annual savings delivered by the project
€113.5K / year M0M3M6M9M12
QCDMS & E
Before After
QualityCostDelivery MoraleSafetyEnvironment
Control: locked in
Standardized
Process changes written into company standards
Weekly risk assessment
Electric-board jigs checked every week
Validated
Site, supplier and Central Engineering approval
Control charts
p-chart on anti-back defects, reviewed every week to keep the process in control
Yokoten: shared across the group
7 SITES
ORIGIN our site EgyptPort SaidEgypt10th of RamadanRomaniaDevaMoroccoKenitraMoroccoAin AoudaMoroccoSkhiratTunisiaMonastir
650
jigs on 12 electric test boards next in line, across CHR, Yaris and Yaris Cross
Download Project Brief Download Full Project Presentation
Automation · Rollc KSA

Automated Fabrication Drawings Platform

I designed and implemented a fabrication drawing system with a direct interface to the production team. Drawing release is now standardized: a product's full drawing set is generated in seconds, and errors no longer reach the shop floor.

1 h → 15 s
Fabrication drawings per product
240×
Faster drawing release
3/26 → 0
Drawings with fabrication errors

Time to produce one drawing set

per product
Manual drafting≈ 60 min
Automated platform15 s

The green sliver is the new time to scale: 15 seconds is 0.4% of the hour it used to take.

Drawing errors, 26 drawings

each tile = 1 drawing
Before3 with errors
After0 errors

Accuracy and precision

target view is illustrative
BEFOREManual Drafting DeskManually preparing fabrication drawings
Every drafter, a different result. Off target and inconsistent.
AFTEROne-Click Drawing EngineFabrication drawings generated automatically
Same rules every time. On target and repeatable.
Accuracydrawings right first time
Before88.5%
After100%
23 of 26 correct before, 26 of 26 after
Precisiondrawings on the company standard
Before90%
After100%
Every drawing is generated from one rule set

How it works

01Product data inDimensions and options for the product
02Drawings generatedStandardized fabrication drawings in about 15 seconds
03Direct releaseSent straight to the production team, with no manual hand-off
04Right first timeZero drawing errors and less scrap on the shop floor